Description
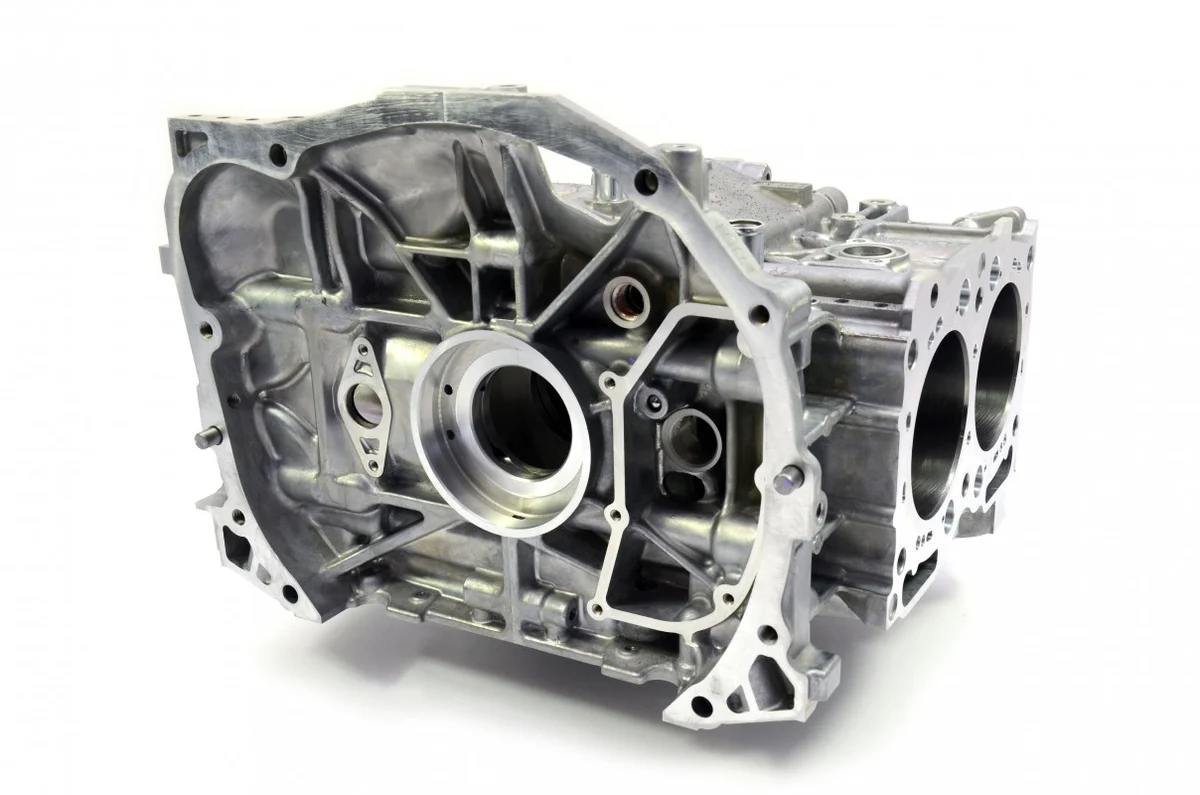
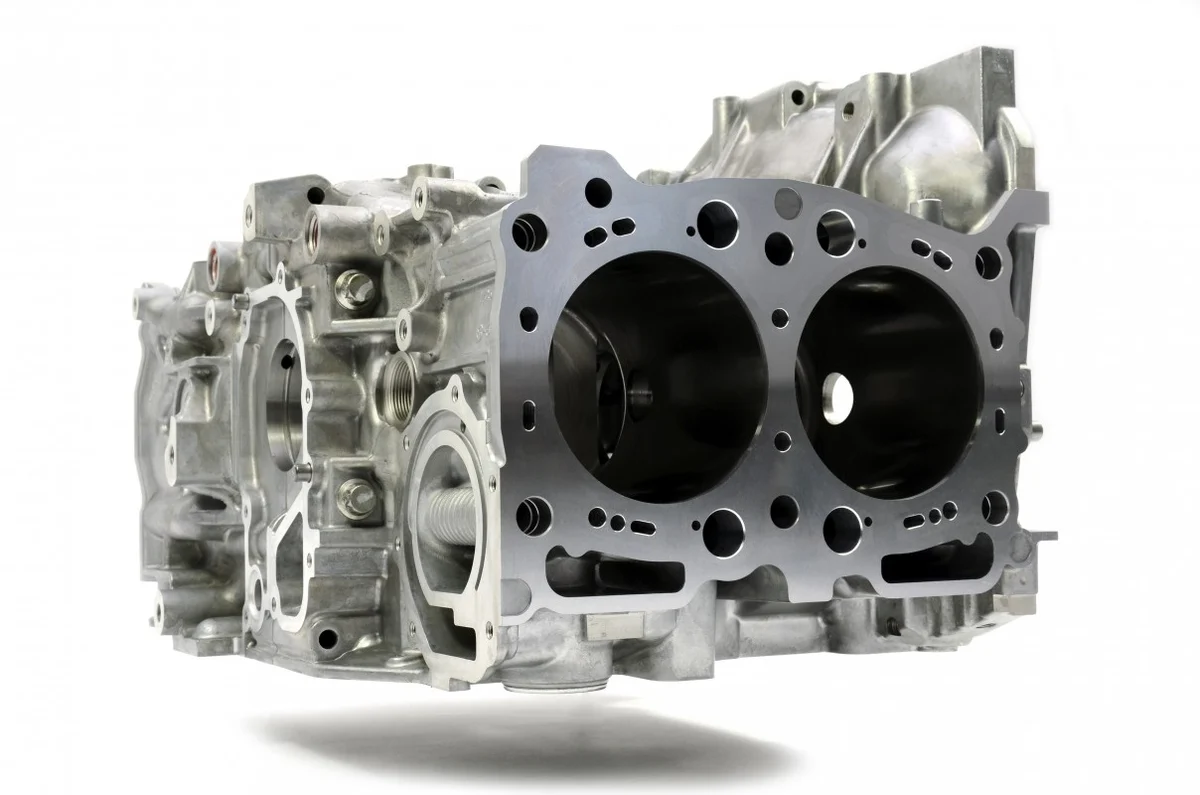
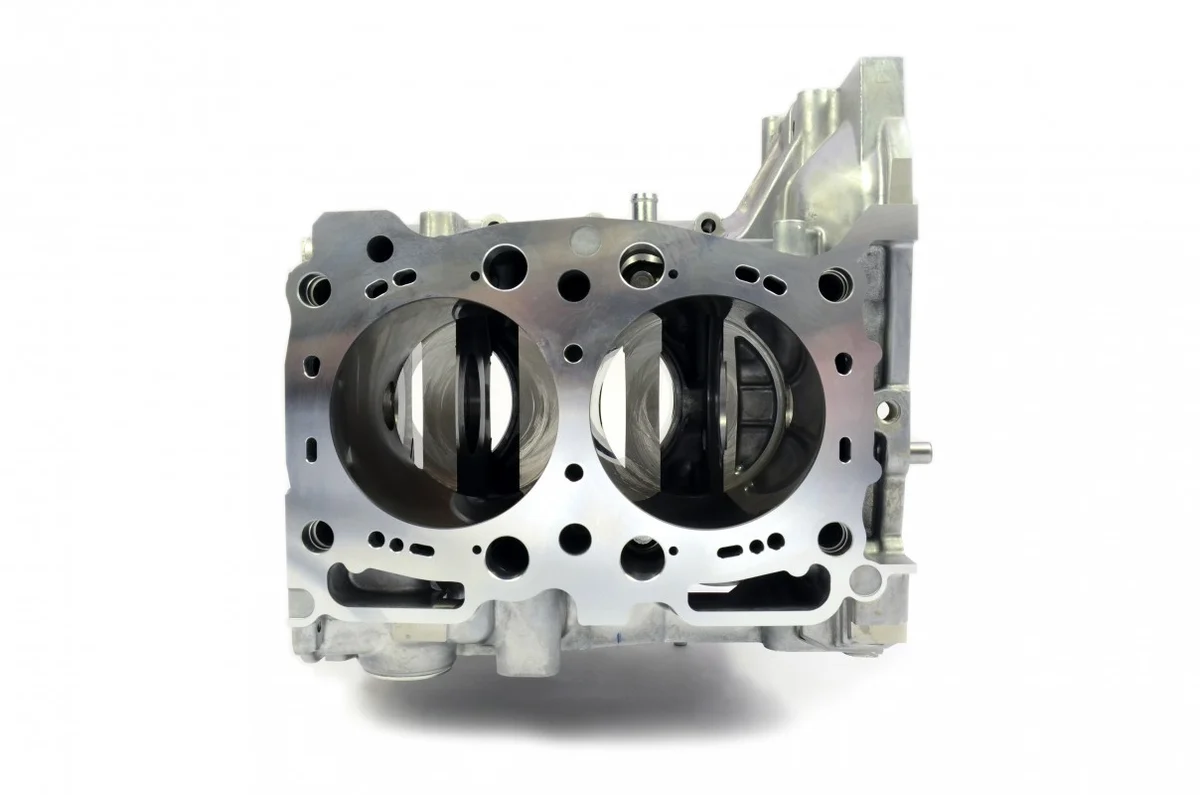
IAG Stage 3 Closed Deck converted case halves are a cost-effective short block modification for Subaru EJ25 turbo engines. The deck surface is machined to accept CNC-cut cast inserts that strengthen the weakest point of the OEM case, at the upper sleeve. Suitable for street or race use.
What is a closed deck block and why is it needed?
The factory EJ25 case has a semi-open (semi-closed) deck: essentially an open deck with 3 narrow supports tying the main case to the tops of the sleeves. This was a slight improvement over the EJ20 case, which was a completely open deck with no support. The supports are there to keep the sleeve from moving, but on a high-horsepower Subaru they are not enough, and the weakest point of the sleeve is still left open.
What is unique about IAG's closed deck process?
The machining process converts the semi-open deck to a fully closed deck, using cast insert material that closely matches the metallurgy of the aluminium case in a factory EJ engine block. With a similar cast material rather than billet, the inserts and case expand and contract at similar rates, which is vital for keeping the top of the bore round. The outer inserts are machined from ¾ inch cast material and the inner inserts from 1 inch cast material. Once the deck is surfaced, the finished outer insert thickness is ½ inch and the finished inner insert thickness is ¾ inch.
The process
The conversion is carried out 100% in-house on a 2015 Haas VF4-SS CNC vertical machining centre, starting with a new OEM EJ25 bare case. The case is fixtured to a 4th axis rotary indexer and supported from the main journals with a precision-ground 2 inch bar and tailstock, so the main journals are the datum for all machining operations. A Renishaw probe confirms the case is fixtured true before machining begins.
- 12 pockets are milled to exact dimensions for the CNC inserts, creating a consistent area to accept them rather than fitting inserts into an inconsistent cast case.
- The case is warmed in a block oven at low temperature while the pre-machined inserts are chilled with dry ice.
- At the desired temperatures, the block is placed in the install station and the inserts are lightly pressed into position on one side of the deck. The process is repeated on the other side, and the case is moved to a cooling rack.
- At room temperature the case is fixtured again and the flanges left from machining the inserts are milled close to the deck surface. Coolant passages and case bolt access positions are machined.
- Finally, each deck surface is machined true and flat with a polycrystalline diamond insert.
Includes
- 1 × IAG Stage 3 Closed Deck converted case halves (new EJ25 case, stock bore 99.5mm)
Boring and honing are required before final assembly. Overbore must be performed before assembly, with 99.75mm the preferred bore.
When using ARP case bolts, IAG recommends line honing the case to remove any distortion created by the hardware. IAG installs ARP case bolts with 30W engine oil, using OEM Subaru torque specs and procedures. Other torque specs and lubricants may lead to case distortion.
Compatible vehicle groups
Compatible model years
- Forester 1996–2002
- Forester 2003–2005
- Forester 2006–2007
- Forester 2008–2013
- Impreza 1992–2000
- Impreza 2001–2002
- Impreza 2003–2005
- Impreza 2006–2007
- Impreza 2008–2013
- Legacy 1992–2003
- Legacy 2003–2009
- Legacy 2009–2014